Hey there! I’m a supplier of vertical conveyor systems, and I’ve been getting a lot of questions lately about the control systems available for these setups. So, I thought I’d sit down and break it all down for you in a no – nonsense way. Vertical Conveyor Systems
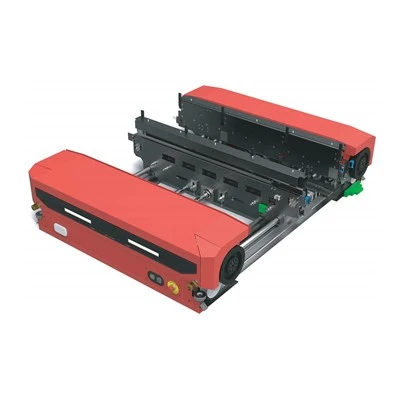
First off, let’s understand why control systems are so important for vertical conveyor systems. A vertical conveyor is designed to move materials up or down vertically, whether it’s in a warehouse, a manufacturing plant, or a distribution center. Without proper control, these conveyors can be inefficient, unsafe, and costly to operate. A good control system ensures smooth operation, precise positioning, and can even help in preventing breakdowns.
Programmable Logic Controllers (PLCs)
One of the most popular control systems for vertical conveyor systems is the Programmable Logic Controller, or PLC for short. PLCs are like the brains of the operation. They’re small, rugged computers that can be programmed to control different functions of the conveyor.
I’ve worked with so many clients who swear by PLCs. Why? Well, for starters, they’re incredibly flexible. You can program a PLC to handle different conveyor speeds based on the type of material being moved. For example, if you’re moving fragile items, you can set the PLC to slow down the conveyor to prevent any damage.
Also, PLCs can manage multiple conveyor operations simultaneously. Say you have a vertical conveyor that has to interface with different horizontal conveyors at various levels. A PLC can coordinate all these movements, ensuring that the products are transferred smoothly.
Another great thing about PLCs is their reliability. They’re built to withstand harsh industrial environments, with features like high – temperature resistance and protection against dust and moisture. And if something goes wrong, most PLCs have diagnostic tools that can quickly pinpoint the problem, saving you time and money on repairs.
Variable Frequency Drives (VFDs)
Next up, we have Variable Frequency Drives, or VFDs. These are essential for controlling the speed of the motors in vertical conveyor systems.
VFDs work by adjusting the frequency and voltage supplied to the motor. This means you can change the speed of the conveyor without having to use mechanical speed – changing devices. And trust me, this is a game – changer.
For one, it provides energy savings. When the conveyor doesn’t need to run at full speed, the VFD can reduce the motor speed, which in turn reduces power consumption. I’ve had clients who’ve seen significant reductions in their energy bills after installing VFDs on their vertical conveyors.
It also extends the life of the motor. By reducing the stress on the motor during startup and operation, VFDs can prevent premature wear and tear. This means fewer motor replacements and less downtime for your conveyor system.
And let’s not forget about the smooth acceleration and deceleration. With a VFD, you can program the conveyor to start and stop smoothly, which is crucial for preventing product damage and ensuring the safety of the operators.
Human – Machine Interfaces (HMIs)
Now, let’s talk about Human – Machine Interfaces, or HMIs. These are the control panels that allow operators to interact with the vertical conveyor system.
HMIs come in all shapes and sizes, from simple push – button panels to touch – screen displays. They give operators real – time information about the conveyor’s status, such as speed, load, and any error messages.
One of the big advantages of HMIs is their ease of use. Operators can quickly adjust settings, monitor operations, and troubleshoot problems without having to be experts in programming. For example, with a touch – screen HMI, an operator can simply tap on the screen to change the conveyor speed or switch between different operating modes.
HMIs also improve safety. They can display emergency stop buttons and safety warnings clearly, making it easy for operators to take action in case of an emergency. And some advanced HMIs can even be integrated with other safety systems, like sensors and alarms, for an added layer of protection.
Sensors and Feedback Systems
No control system for vertical conveyor systems would be complete without sensors and feedback systems. These components are like the eyes and ears of the conveyor.
Sensors can be used to detect the presence, position, and movement of products on the conveyor. For example, photoelectric sensors can detect when a product has reached a certain point on the conveyor and send a signal to the control system to stop or start an operation.
Proximity sensors are also very useful. They can detect the presence of objects in close proximity to the conveyor, which is important for preventing collisions and ensuring safe operation.
Feedback systems, on the other hand, provide information about the performance of the conveyor. For example, encoders can measure the speed and position of the conveyor belt or chain and send this information back to the control system. This allows the control system to make adjustments in real – time, ensuring that the conveyor operates at the desired speed and position.
Safety Control Systems
Safety is always a top priority when it comes to vertical conveyor systems. That’s why safety control systems are so important.
These systems can include things like emergency stop buttons, safety光幕s (light curtains), and interlocks. Emergency stop buttons are, of course, used to quickly stop the conveyor in case of an emergency. They’re usually placed in easily accessible locations around the conveyor.
Safety光幕s are curtains of infrared light that are placed along the sides of the conveyor. If an object or a person breaks the light beam, the safety光幕 sends a signal to the control system to stop the conveyor immediately.
Interlocks are used to prevent the conveyor from operating when certain conditions aren’t met. For example, an interlock can prevent the conveyor from starting if a safety guard is open.
Choosing the Right Control System
Now that we’ve covered the different types of control systems available for vertical conveyor systems, you might be wondering how to choose the right one for your needs.
Well, it really depends on a few factors. First, consider the complexity of your conveyor system. If you have a simple setup with just one vertical conveyor, a basic control system with a PLC and some sensors might be enough. But if you have a more complex system with multiple conveyors, interfaces with other equipment, and high – volume throughput, you might need a more advanced control system with HMIs, VFDs, and sophisticated safety features.
Another important factor is your budget. Control systems can vary widely in price, from a few hundred dollars for a basic sensor to tens of thousands of dollars for a fully integrated PLC – based system with HMIs and VFDs. You need to find a balance between your requirements and your budget.
And don’t forget about the level of support and maintenance. Make sure you choose a control system that comes with good technical support from the manufacturer. You also want to consider the ease of maintenance, as you’ll want to minimize downtime in case of a breakdown.
Let’s Talk
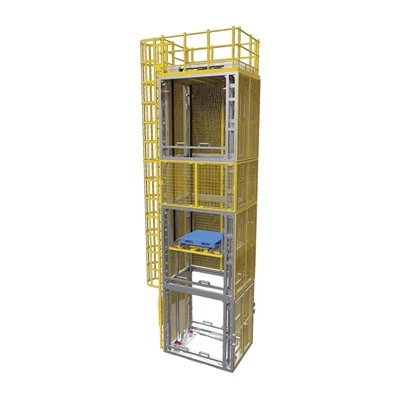
If you’re in the market for a vertical conveyor system and are still unsure about the control systems, I’d love to have a chat with you. As a supplier with years of experience, I can help you figure out the best control system for your specific needs. Whether you’re a small business looking to automate a simple process or a large corporation in need of a high – performance conveyor system, I’ve got the expertise to assist you.
Material Handling Equipment So, don’t hesitate to reach out, and let’s start a conversation about how we can make your vertical conveyor system work better for you.
References
- "Automation in Conveyor Systems" by Smith, J.
- "Conveyor Control and Safety" published by the Industrial Automation Association.
- "Variable Frequency Drives: Principles and Applications" by Brown, A.
Anhui Rayo Automation Technology Co., Ltd.
With abundant experience, we are one of the most professional vertical conveyor systems manufacturers and suppliers in China. Please feel free to wholesale advanced vertical conveyor systems in stock here and get quotation from our factory. All customized products are with high quality and competitive price.
Address: No.28 Yongzhen Road, Wuhu Area, China (Anhui) Pilot Free Trade Zone
E-mail: ahry@ahrayo.com
WebSite: https://www.rayosmart.com/
